Our Research and Development team drives continuous improvement and innovation, developing new recipes, refining production methods, and ensuring F2F stays ahead of market trends and evolving dietary demands.
It is the engine behind our 300-plus product portfolio, and the reason our clients can move from concept to shelf-ready product with one accredited partner.
Products Developed
Driven by Research
Quality & Food Safety
From Concept to Shelf Ready
Our food technologists manage shelf-life and quality testing to ensure product stability, safety and performance across the supply chain, along with competitor and pricing analysis that keeps every product commercially sharp as well as technically sound.
Every F2F product starts as a bespoke recipe, formulated by our food production specialists to align with evolving tastes and nutritional trends, then proven for consistency at high-volume production scale. This is how we deliver restaurant-quality flavour whether the batch is fifty units or fifty thousand.
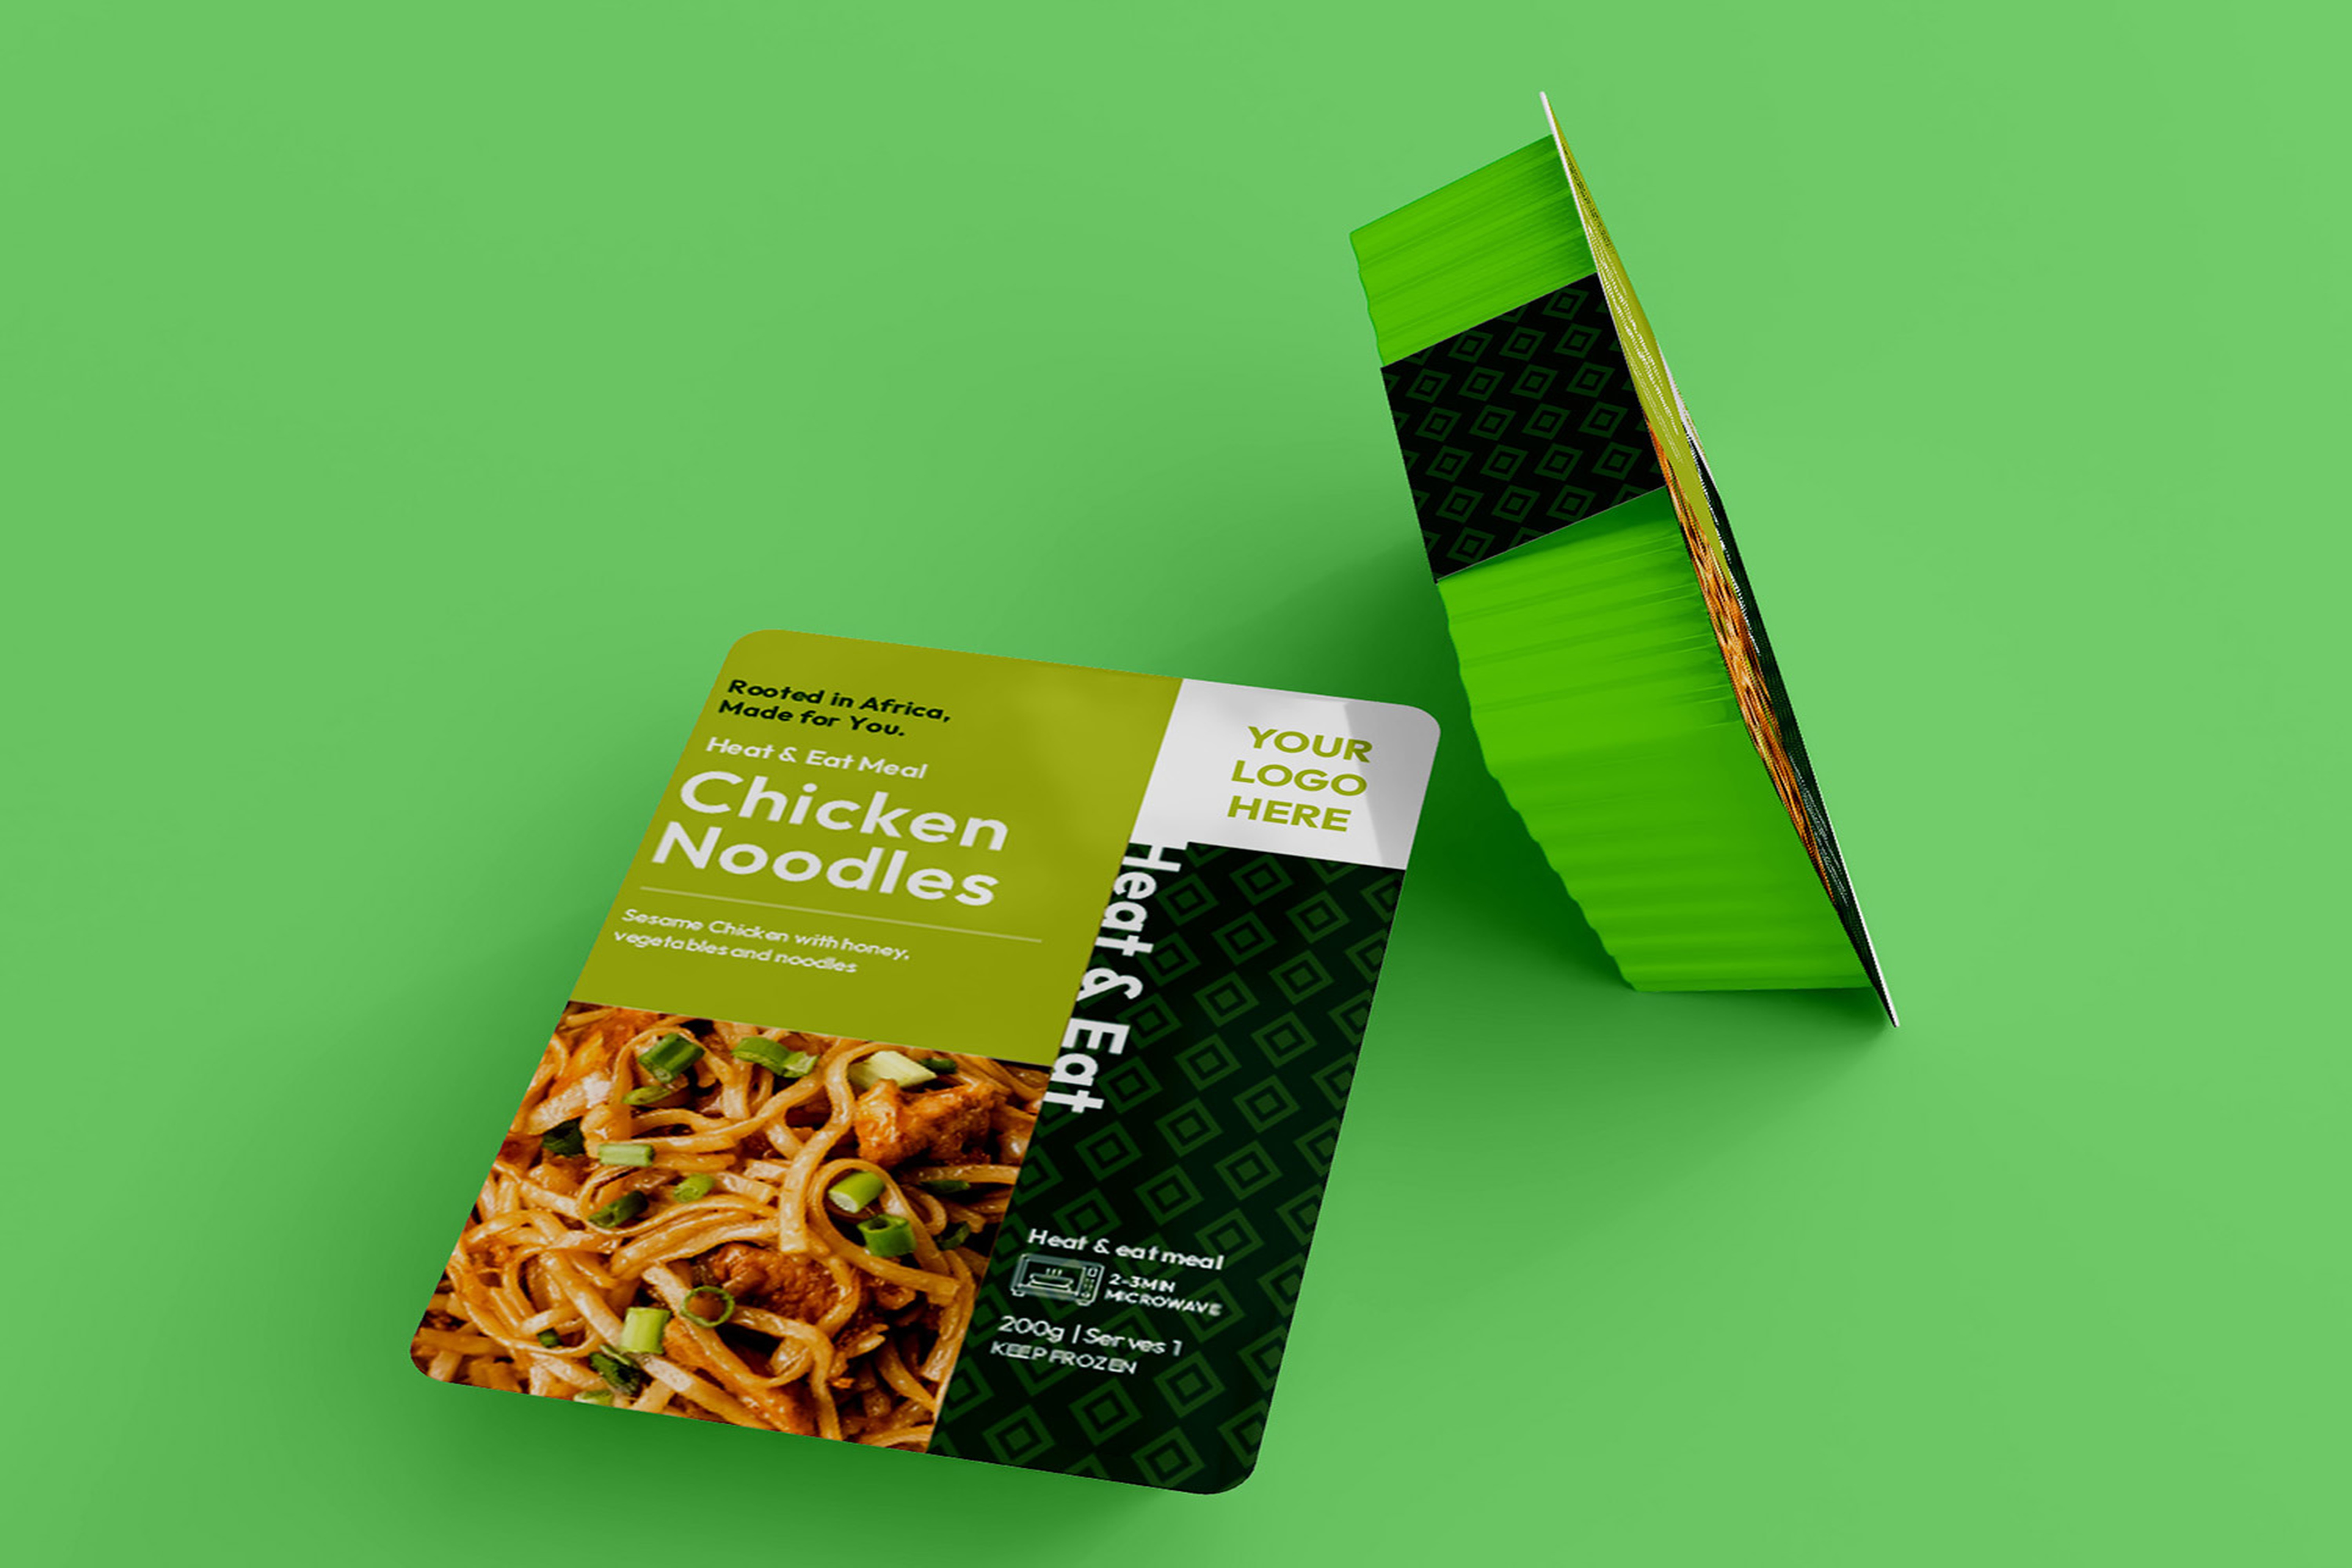
Our packaging specification design covers everything from functional cold-chain performance to shelf appeal, alongside full brand and concept development to give new products a strong identity and clear market positioning from day one.
Our R&D team is committed to creating smarter food solutions that keep our clients ahead of evolving consumer needs.